NELSON F150 Sprinkler

*Images for illustrative purposes only.

The Nelson F150 is a high-volume impact sprinkler designed for large-scale irrigation projects requiring superior throw range and extreme durability. Its unobstructed flow-path design allows it to handle water containing suspended particles without clogging, while its smooth rotation mechanism ensures uniform, consistent water distribution for full-coverage applications, pastures, and industrial dust control.

Specifications:

  • Min. operating pressure: 50 psi
  • Max. operating pressure: 100 psi
  • Min. flow rate: 100 GPM
  • Max. flow rate: 229 GPM

Related Products

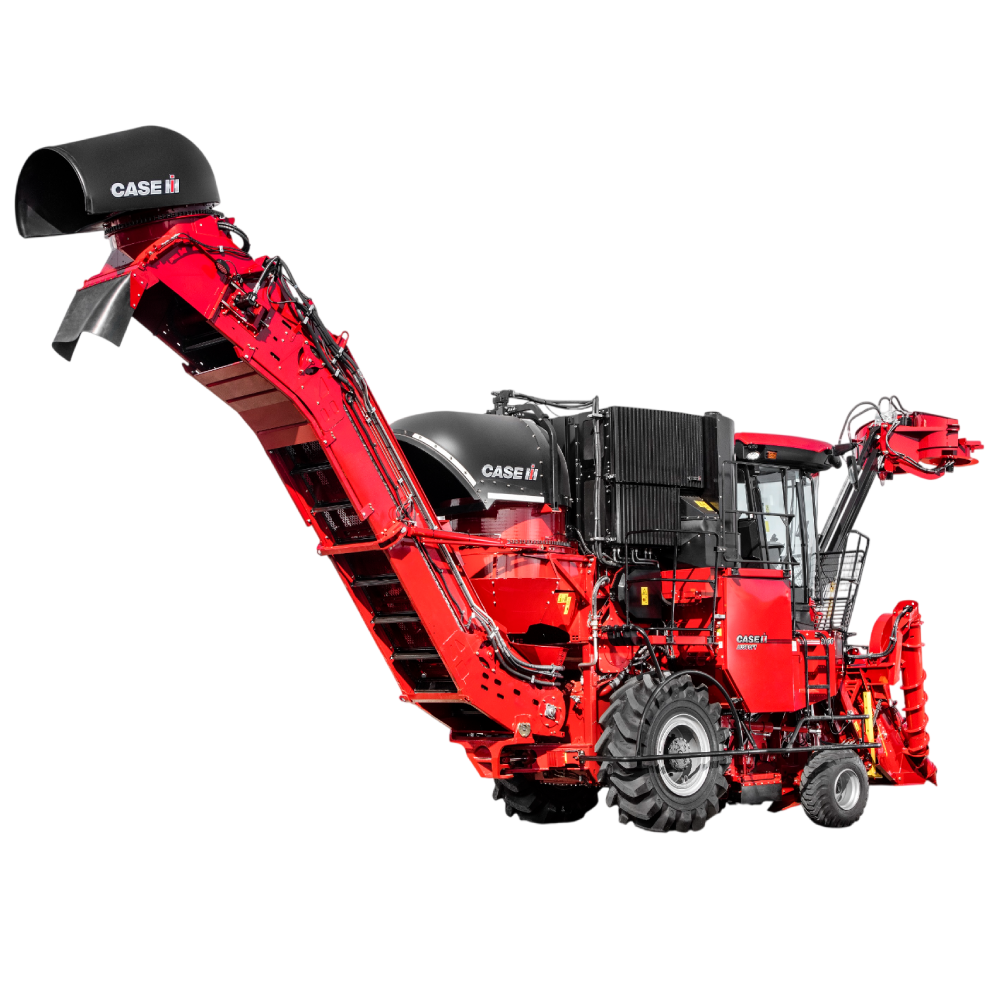
Sugar Cane Harvester CASE AUSTOFT 9000

The high performance of CASE IH sugar cane harvesters is the result of more than 50 years of research, product development, and a continuous commitment to offering advanced solutions to the sector. The technological innovations of our harvesters ensure high productivity and availability, guaranteeing the delivery of raw material that meets industry specifications. CASE IH is globally recognized as a pioneering brand and leader in the sugar cane segment. We create and set the standards in agricultural technology.

Specifications:

  • Engine: CASE FPT Cursor 11, 6-cylinder
  • Power: 415 HP
  • Configuration: Wheeled

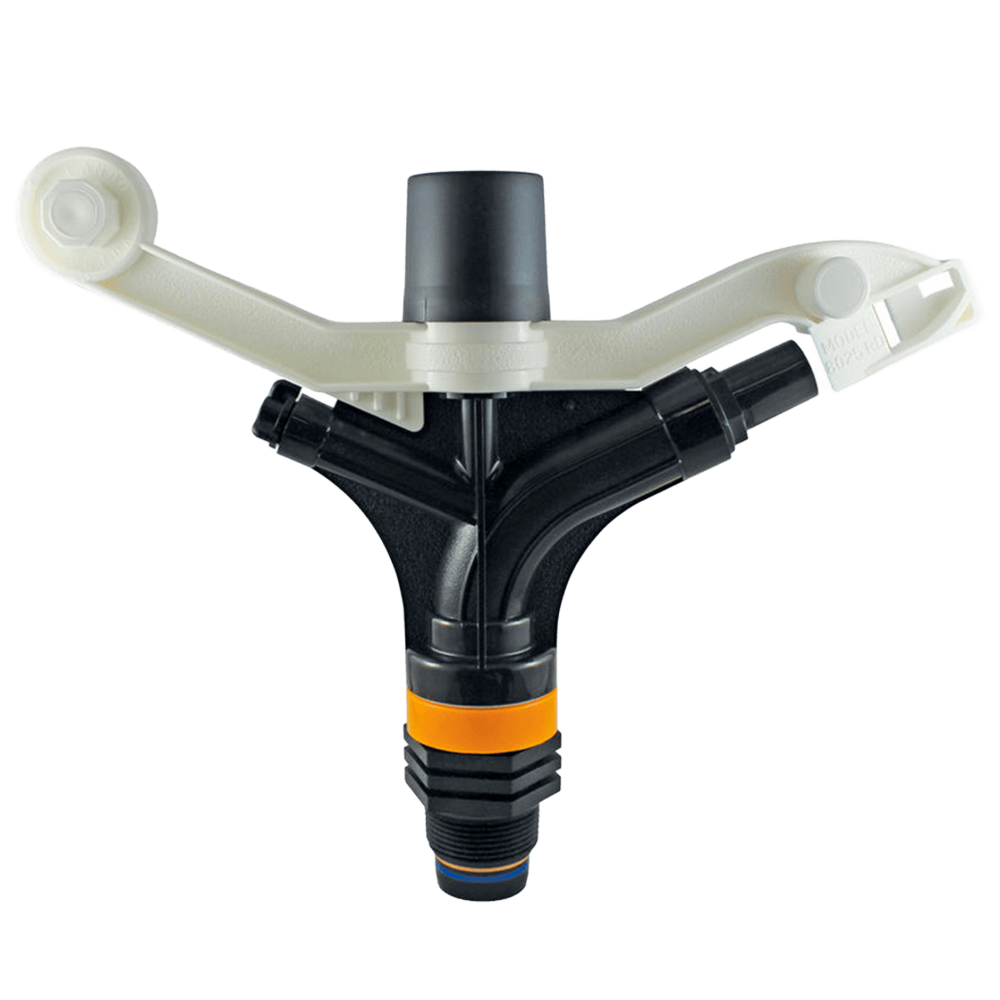
8025 Mini-sprinkler

The Senninger 8025 is a high-performance impact sprinkler for large-scale agriculture, designed to handle high-volume flow rates with superior efficiency. Its 25° trajectory ensures the ultra-long throw required to optimize irrigation designs with wide spacing, while its engineered thermoplastic construction offers complete resistance to corrosion and chemical wear under the most demanding conditions.

Specifications:

  • Min. operating pressure: 40
  • Max. operating pressure: 70
  • Min. flow rate: 5724 L/h
  • Max. flow rate: 23,439 L/h

Rovatti Centrifugal Electric Pump

The Rovatti submersible multistage centrifugal electric pump is the ultimate solution for water extraction from deep wells and reservoirs where high pressure and consistent performance are required. Its compact, sealed design, combined with multistage technology, enables the lifting of large flow rates with superior energy efficiency, ensuring reliable operation and a long service life even under continuous duty conditions.


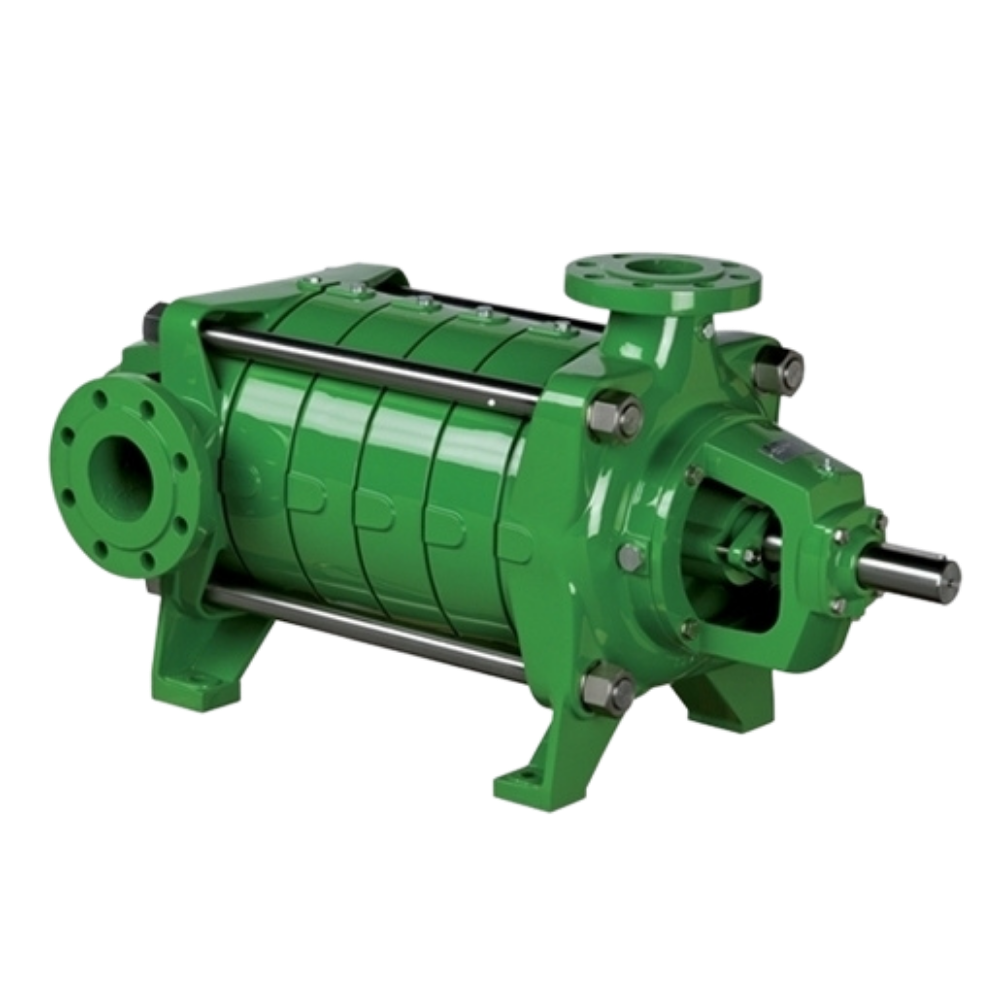
Rovatti Bomba Centrifuga

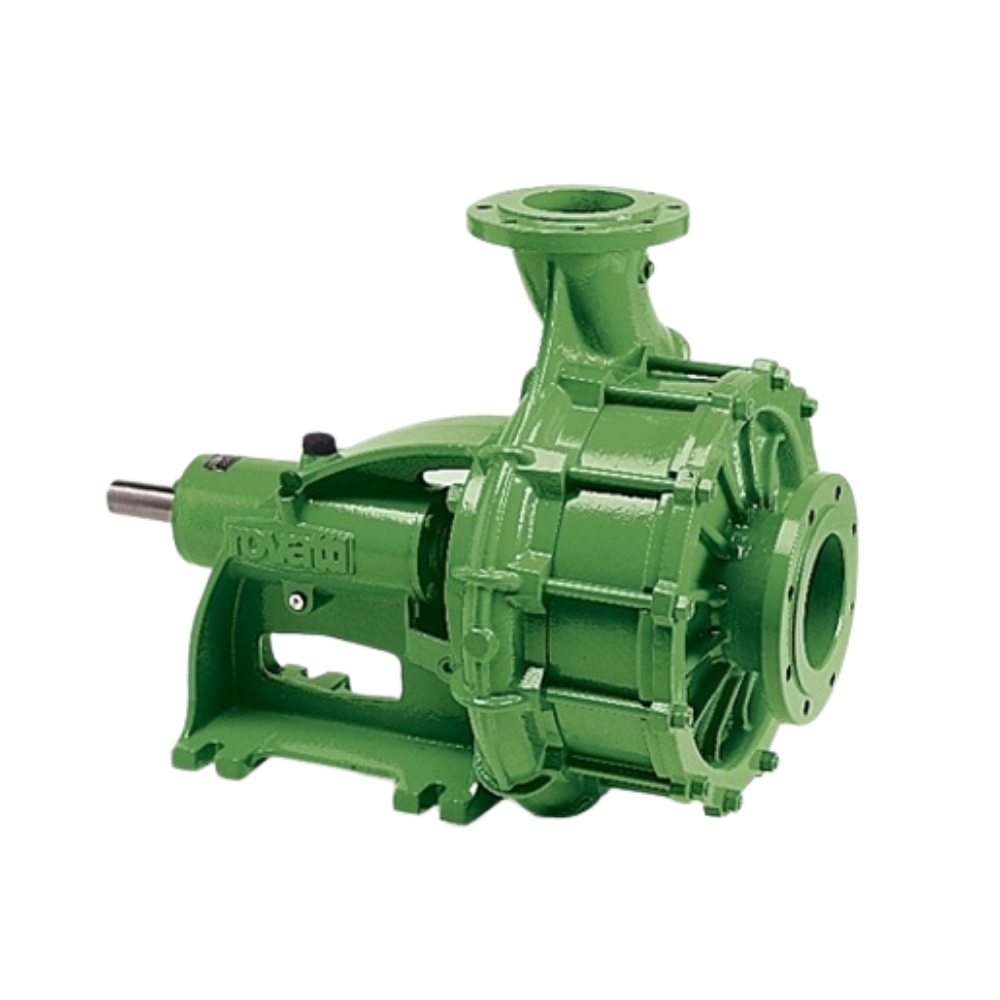
The Rovatti horizontal multistage centrifugal pump is specifically designed for applications requiring high pressure and maximum efficiency. Its multistage configuration enables high lift heads with constant flow, making it the ideal solution for sprinkler irrigation systems, industrial processes, and supply networks that demand power, durability, and exceptional hydraulic performance.